◆ Clay
Fluted tumbler slip casting mold
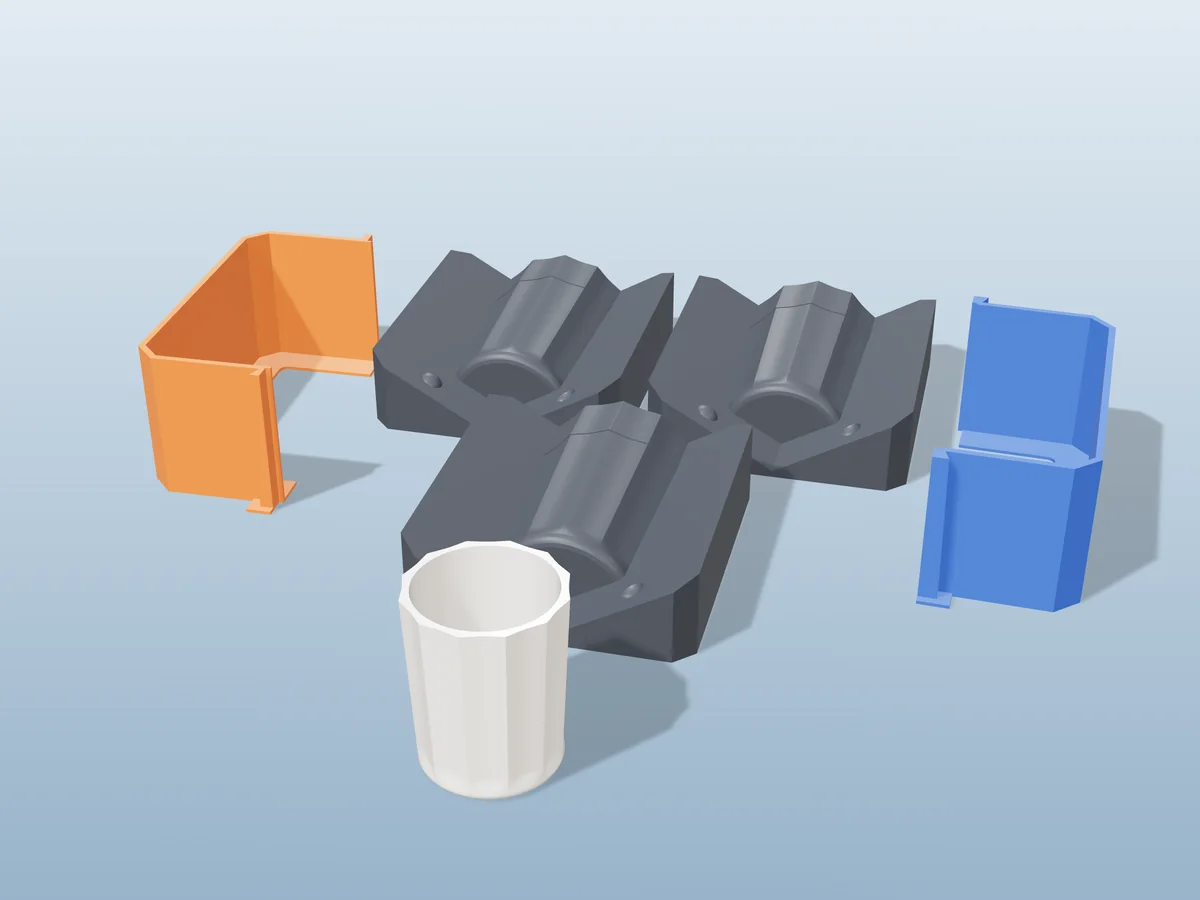
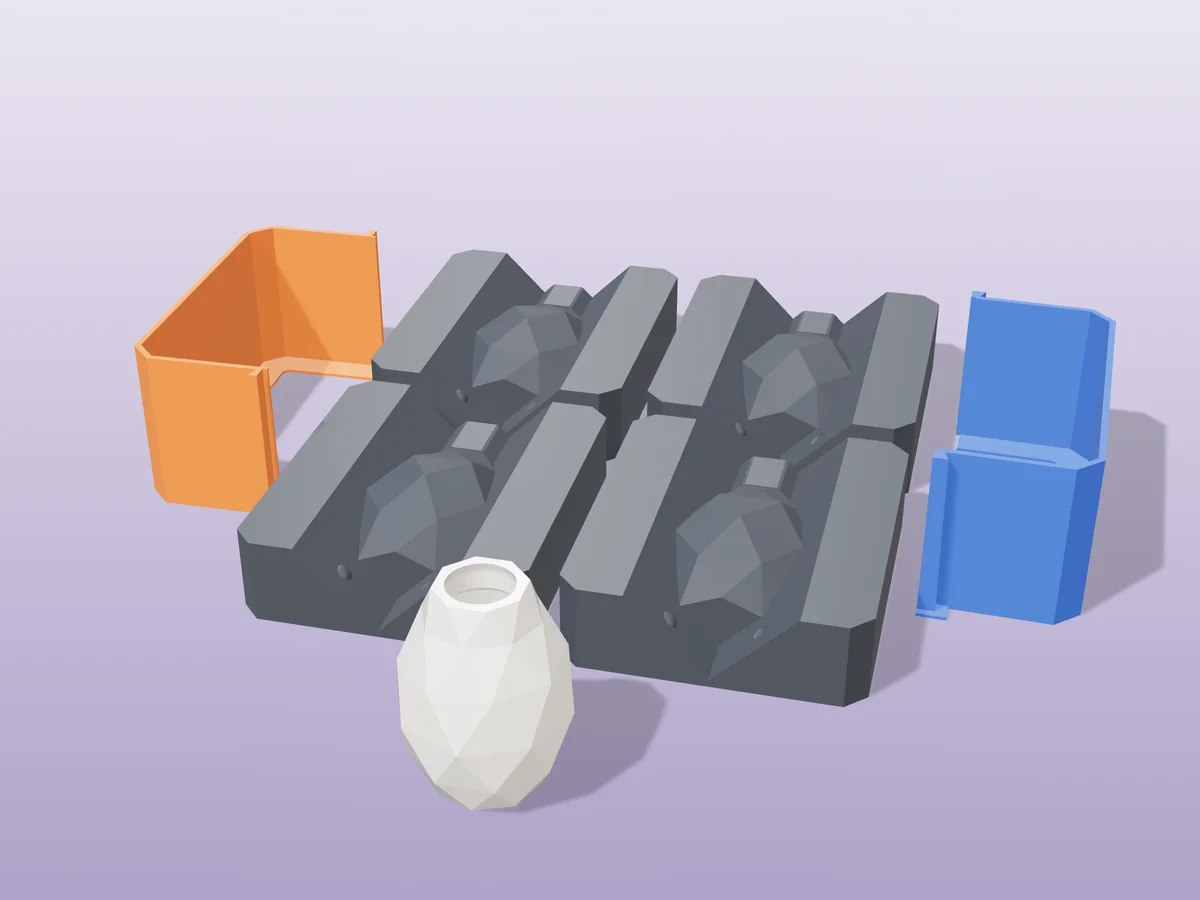
A three-piece plaster mold for slip casting a fluted 323 ml tumbler with twelve crisp flutes.
◆ Clay
A three-piece plaster mold for slip casting a fluted 323 ml tumbler with twelve crisp flutes.
A tumbler 82 mm across and 100 mm tall once fired, with twelve concave flutes running up from the foot and sharp ridges between them. It holds 323 ml to the brim. Fluted cups are one of the most searched slip casting shapes, and glaze pooling in the flutes does the decorating for you.
Made with our plaster mold generator: a printed housing per plaster piece, you pour the plaster, and the plaster is the mold. It is a three-piece mold. The page's seam check found nothing stuck at two pieces either, but at two the flute walls next to each seam run straight along the pull and scrape as the plaster comes off; at three, four flutes to a piece, every flute wall has draft. Open at the rim, mold cut 15% oversize for a 13% shrinkage slip.
The zip carries the three bases, one shell and clamp set that fits all three, the tumbler as its own STL, the tool's print sheet and a recipe file for the generator.
Shown as a 3D render of the printed bases and shells with the fired piece in front, not a photo.
Print the 3 bases and the one set of shells and clamps, no supports. The sheet in the zip asks for 4 or more walls and 40% gyroid, because the shells get clamped.
Stand the two shells round the first base, slide the clamps over the ends, and run a thin bead of petroleum jelly along every seam. Brush mold soap over the printed master slice and the natch sockets so the plaster lets go.
Sift pottery plaster into water (about 100 g of plaster to 70 g of water), let it slake for two minutes, mix for three, then pour it up to the top of the shells and tap the housing to lift the bubbles.
After 30 to 45 minutes, when the plaster is warm and hard, unclamp, lift the shells off and ease the plaster piece off the base. Move the same shells and clamps to the next base and pour again.
Let the plaster pieces dry for about a week somewhere warm and airy, until they feel light and no longer cool to the touch. A damp mold barely takes water out of the slip.
Band the 3 pieces together with the natches seated, stand the mold mouth up and fill it to the brim with slip. Top it up as the level drops.
When the wall is 3 to 4 mm thick (usually 10 to 20 minutes, check at the rim), pour the slip back out and leave the mold upside down to drain.
Once the cast loses its shine and pulls away from the plaster, trim the rim, open the mold and lift the piece out. Dry it slowly to bone dry, then bisque and glaze fire.
Print details
| Cast material | Clay |
|---|---|
| Printed parts | 7 |
| Size (W x D x H) | 175 x 219 x 92 mm |
| Print bed needed | 219 x 164 mm, 93 mm tall |
| Filament | ~2534 g |
| Layer height | 0.2 mm |
| Infill | 40% |
| Supports | Not needed |
| Download | ZIP: 3 bases + one shell and clamp set (7 printed parts, STL) + tumbler master (STL) + print sheet + recipe |
| Added | 2026-09-25 |
Pro early access until October 25, 2026, then free with any account.
Make your own plaster slip-cast mold →Made with the free Plaster slip-cast mold generator. Upload your own model and get the same kind of mold built around it, in your browser.
Free for personal use. Selling the pieces you cast needs a commercial licence (Pro or Founder); passing on the file itself is not permitted on any plan. Full terms.
New to casting? Read the plaster mold guide.
Yes, and the natches will not tell you: every seam carries the same ball and socket, so any piece seats in any position. Number each piece in pencil on the outside as it comes off its base (base 1, 2, 3) and always band them together in that order.
The seams fall on the ridges between the flutes, where a faint line disappears into the edge. At leather hard, run a damp sponge or a soft rib along each ridge once. Do not scrape: the ridge is the detail, and it is easy to round off.
A breaking glaze, one that runs thin over edges and pools thick in hollows. Celadons, tenmokus and most satin glazes with some flow do it. The ridges come out pale and the flutes dark, with no painting at all.
 ClayPro early access
A two-piece plaster mold for slip casting a 114 ml espresso cup. Print the housings, pour the plaster, cast.
 ClayPro early access
A two-piece plaster mold for slip casting a 365 ml straight mug body. Add your own pulled or cast handle.
 ClayPro early access
A two-piece plaster mold for slip casting a 115 mm bud vase: round bulb, long neck, rolled lip.
 ClayPro early access
A two-piece plaster mold for slip casting a 116 mm matcha bowl (chawan) with a small foot.
 ClayPro early access
A three-piece plaster mold for slip casting a hexagonal bottle vase with a sloped shoulder and hex neck.
 ClayPro early access
A three-piece plaster mold for slip casting a ribbed 72 mm Christmas bauble with its hanging neck.
 ClayPro early access
A four-piece plaster mold for slip casting an eight-lobed pumpkin votive or jar, 110 mm across.
 ClayPro early access
A four-piece plaster mold for slip casting a low-poly faceted vase, 122 mm tall with triangle facets.